A chain does not want fifty stores. It wants one store, built fifty times. That distinction is the whole discipline of retail fixture manufacturing — and it is why a rollout is a production program, not a series of fit-outs.
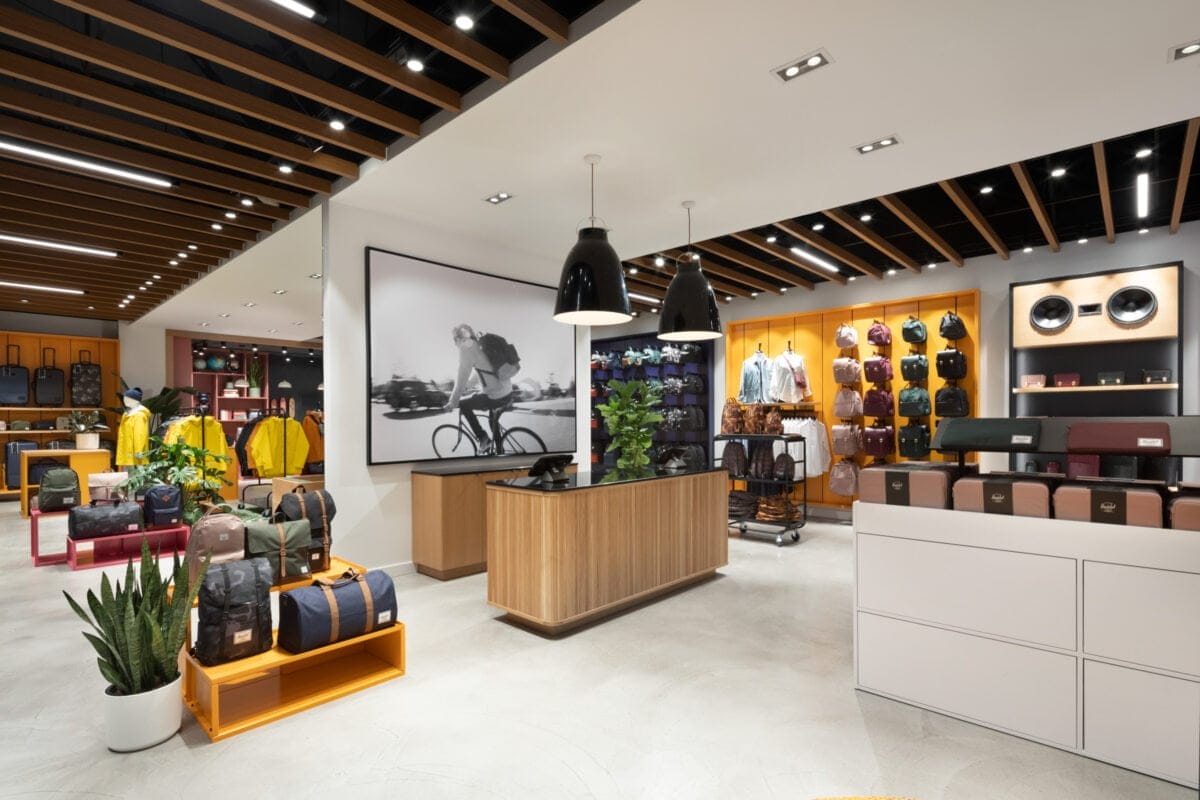
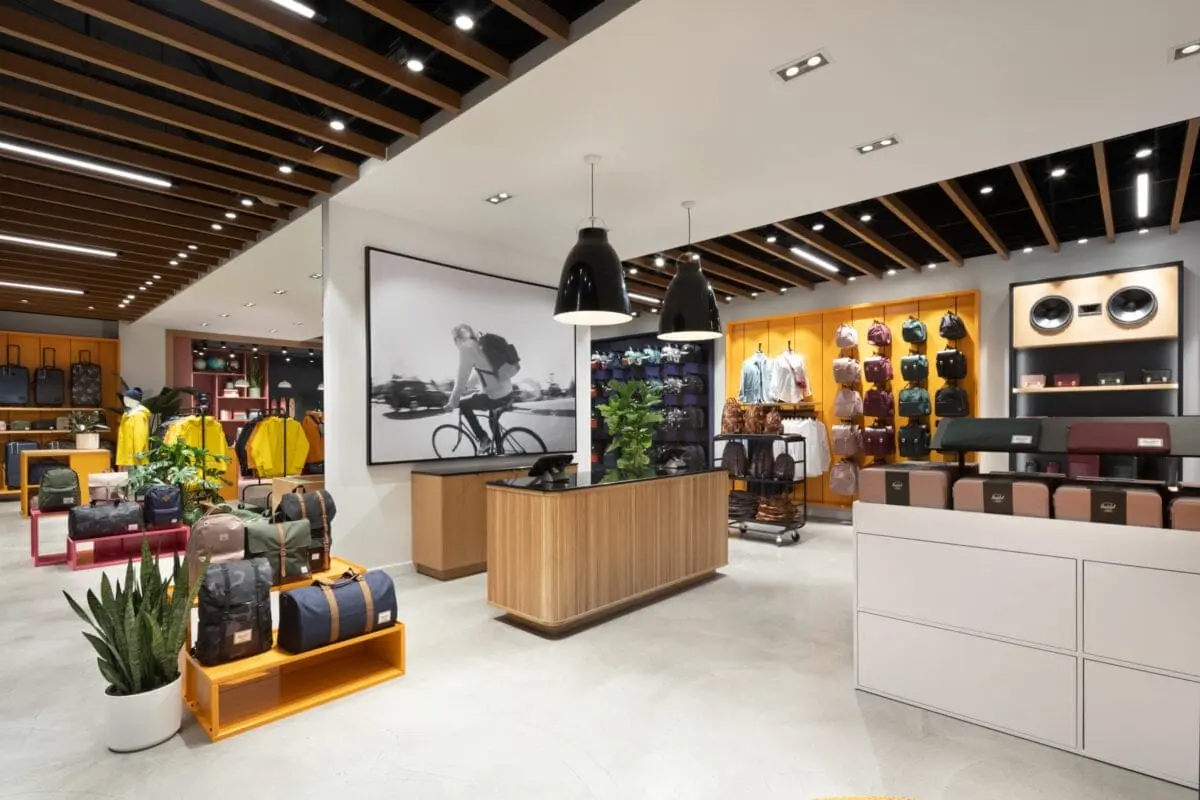
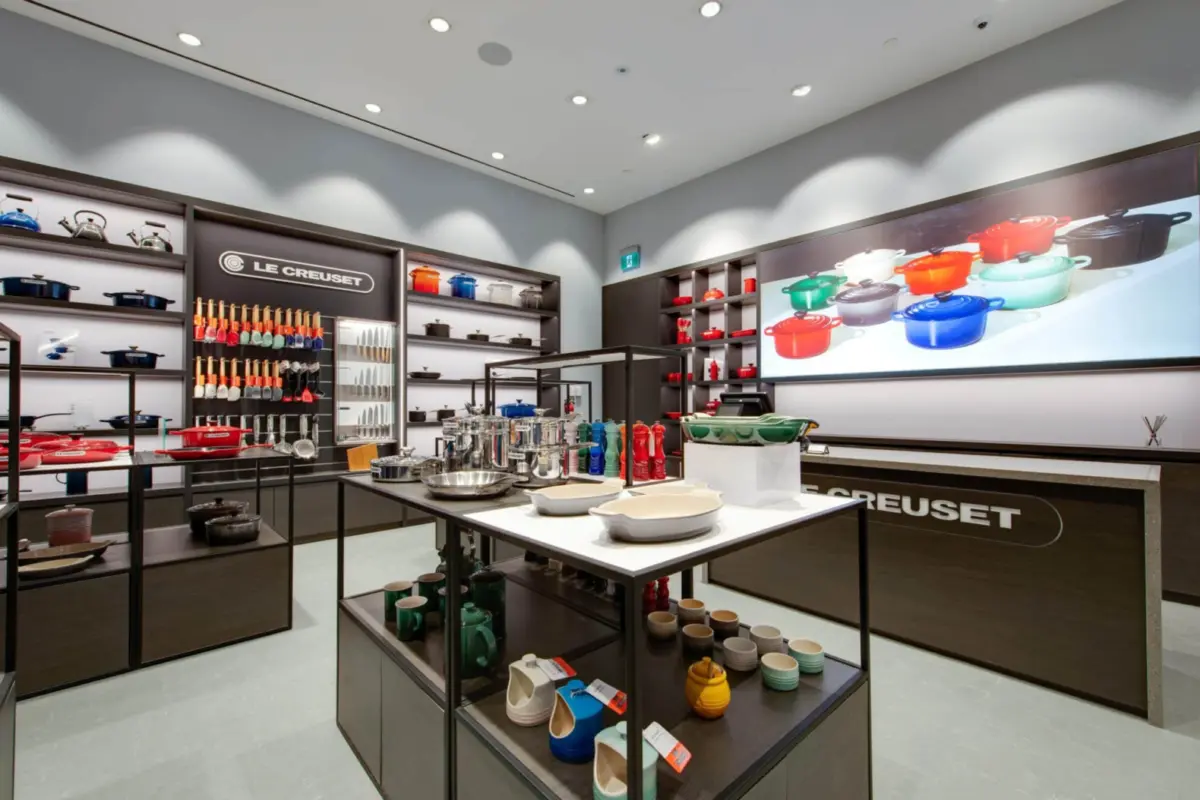
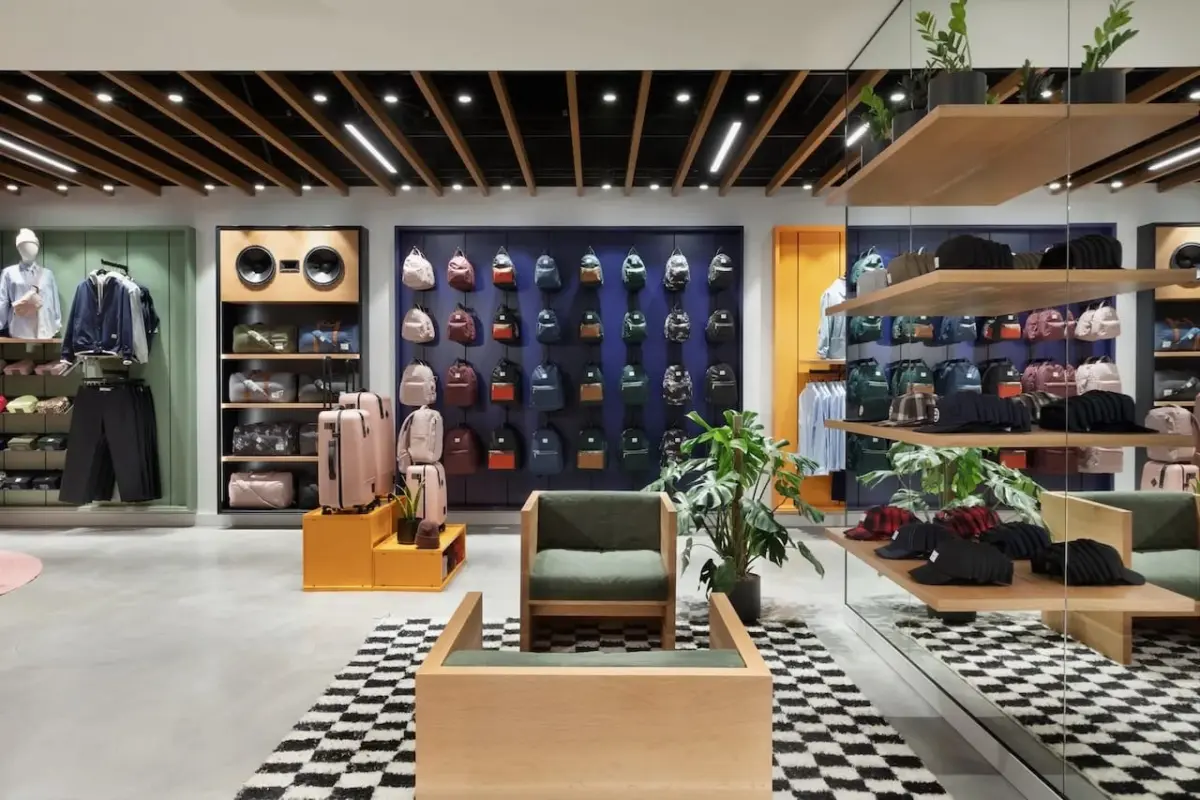
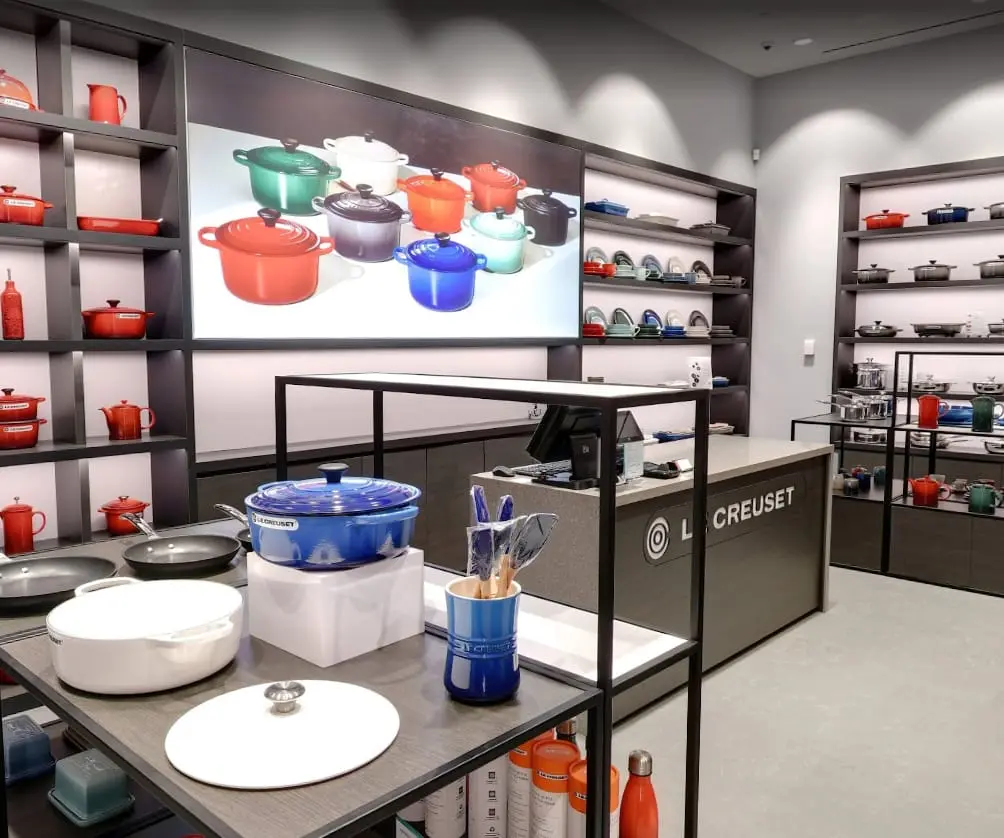
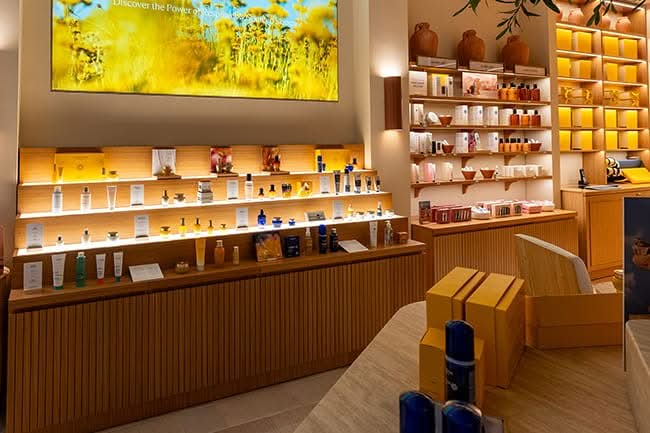
DNS Industries manufactures store fixtures and retail millwork for national and international brands, including L’Occitane, Herschel Supply Co., Le Creuset, Mango, Uniqlo and King Living. DNS is the millwork supplier of record for L’Occitane North America and has produced more than 60 L’Occitane stores — the same store, built to the same standard, sixty times over. In cannabis retail, a separate segment, DNS has fixtured more than 350 locations. Multi-location production at volume is the core of what this shop does, not an adjacent service.
Two other program types run through the same floor. We also produce the BSH and Bosch appliance display program that rolls out inside Best Buy, Home Depot, RONA, Sleep Country and The Brick — shop-in-shop builds where one brand standard has to hold across five host retailers, each with its own site rules, install windows and store conditions. And as direct-to-consumer brands open physical space, DNS builds the showrooms they open with — King Living, Silk & Snow and, most recently, Cozey.
Pilot, standardize, scale
The model that makes a rollout predictable:
- Pilot. We build one reference store to the design. Materials, finishes, construction and cost are proven on a real unit the brand can walk into — not approved from a rendering.
- Standardize. The approved unit becomes a production package: shop drawings, a fixed bill of materials, locked finish sources. This is the step brands most often skip, and the one that determines whether store forty matches store one.
- Scale. Units are produced in runs, kitted per location, and shipped to each opening date.
Why per-store cost falls — and by how much it shouldn’t
Drafting, shop drawings and machine setup are one-time costs spread across the whole program. Repeat runs are faster than first builds. So a fifty-store program is never fifty times the cost of one store.
What it should not do is fall by cheapening the build. A per-unit price that drops because the substrate got thinner or the edge treatment changed is not economy of scale — it is the fixture quietly getting worse, which shows up as replacement cost in year three. (See value engineering for the difference.)
Consistency is a supply chain problem, not a drawing problem
Brand consistency across locations fails in predictable ways, and almost none of them are design failures:
- Finish drift — a laminate or veneer re-sourced mid-program from a different supplier, in a slightly different lot
- Substitutions between runs — hardware discontinued, replaced with “equivalent”
- Multiple fabricators — two shops building the same drawing produce two different results, because drawings do not encode shop practice
- No controlled reference — nothing physical to measure store forty against
Locking the bill of materials and assembling the fixtures in one facility is what prevents this. It is also why first article approval matters more on a rollout than on any single project — one error, caught once, instead of repeated fifty times.
Logistics is part of the manufacturing scope
On a rollout the fixture package has to arrive at the right store, in the right week, in the right order to be installed. That means kitting per location, staging finished units until the site is ready, and sequencing deliveries against an opening calendar that will move.
Storage is the part nobody prices. Store openings slip — and finished fixtures have to live somewhere while they do. Building that into the program at the start is cheaper than negotiating it at the fourth delay. (See stored materials and off-site fabrication.)
Speed to opening
Retail revenue starts on opening day, and every week of delay is rent against zero sales. That makes fixture lead time a commercial number, not a schedule number — and it is the reason the pilot should be built well before the rollout calendar is set, rather than in parallel with it.
What we build
- Cash wraps and service counters — POS-integrated, the highest-wear fixture in the store
- Display systems and merchandising walls — reconfigurable as the assortment changes
- Feature millwork — the brand moments that make a space photograph
- Fitting rooms and back-of-house casework
- Cross-material assemblies — wood, metal, glass, solid surface and integrated LED on one set of shop drawings and assembled in one plant before delivery. That matters because a display case is all four at once
See also: custom display fixtures, retail store fixtures for Toronto and the GTA, store fixture manufacturing across Ontario and store fixtures for US brands opening in Canada.
Recent retail projects: L’Occitane North America program, Herschel Supply Co., Le Creuset with SAJO and Pout with Carbon Building Group.
Frequently asked questions
What is a retail fixture rollout program?
A rollout treats a chain’s fixtures as one manufacturing program rather than a series of one-off builds — pilot store approved, package standardized into production drawings and a fixed bill of materials, then units produced, kitted and delivered store by store.
Why does per-store fixture cost fall on a rollout?
Drafting, shop drawings and setup are one-time costs spread across every location, and repeat runs are faster than first builds. The first store carries the drafting; every store after is cheaper.
How does DNS keep fixtures consistent across locations?
By locking a reference unit, fixing the bill of materials and finish sources, and producing every location on the same equipment in the same facility.
How many locations has DNS rolled out?
More than 60 stores for L’Occitane, for whom DNS is the millwork supplier of record in North America, and more than 350 cannabis retail locations across North America. Rollout volume, not one-off fabrication, is the core of the business.
Planning a store program or rollout? Send us your drawings →